
 Switzerland
 Poland

 Czech Republic
 Germany


 Spain
UltraStar X25
New-generation cross-flow ultrafiltration with high performance, flexible membrane selection and advanced automation

Tubular ultrafiltration for high product yield, and flexible membrane selection
- High product yield and net operation time with low product losses
- Wide-bore tubular membranes for high suspended solids tolerance and high retentate concentration
- Wide choice of membrane and module configurations from leading manufacturers for greater process flexibility
- Compact Units with small footprint and outstanding hygienic design
- Fully automatic production and CIP programs with inline pH control
- High operational safety through monitoring and control of all relevant process parameters and hydraulic design for maximum membrane protection
- Sophisticated management of up- and downstream tanks
- High-quality components and maintenance-friendly design for reliable long-term operation
Cross-flow ultrafiltration for food, beverage and biotechnology applications
The UltraStar X25 has been designed for applications in the food industry and biotechnology. Typical applications include fruit juices, fruit wines, vegetable juices, plant extracts and fermenter broths.
Wide-bore tubular membranes with an internal diameter of 12.7 mm (1/2’’) provide high suspended solids tolerance and allow high retentate concentration.
Cross-flow ultrafiltration with advanced process control and fully automatic CIP
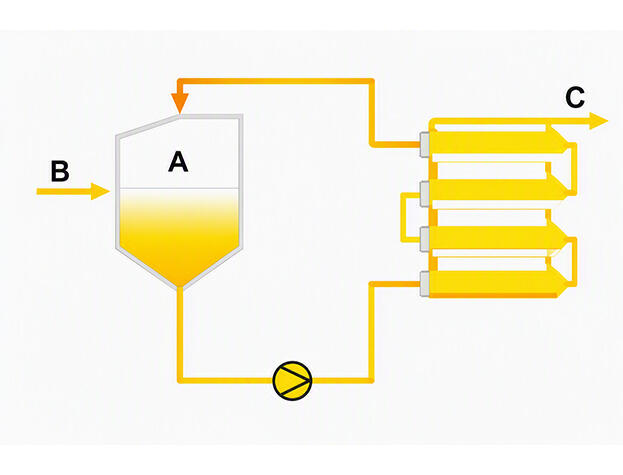
The UltraStar X25 is a semi-continuous cross-flow ultrafiltration system. During production, fresh feed (B) is continuously added to the circulation tank. The retentate (A) is recirculated through the ½” tubular membranes, flowing tangentially along the membrane surface. A transmembrane differential pressure drives part of the liquid through the membrane as permeate (C), while suspended and colloidal components are retained in the retentate. As permeate is removed, the retentate is progressively concentrated. Once the target concentration is reached, diafiltration can be used to recover membrane-permeable dissolved components and further improve product yield.
The vertical arrangement of the retentate piping reduces the footprint and avoids dead legs. Production and CIP programs are fully automatic, while sophisticated control of critical process parameters supports safe and reliable operation. The system combines this advanced process control with user-friendly operation and visualisation. The automatic valve batteries eliminate manual pipe changeover when switching to CIP, and inline pH measurement enables pH-controlled caustic dosing. Optional tank management can control up to 10 upstream and 6 downstream tanks. The control system also acquires and provides comprehensive process data to support production managers. Membranes from leading manufacturers can be selected for different applications.
| Membrane modules | 37 membrane tubes per module, 3.6 m long, 5.2 m² membrane area per module; transparent plastic or stainless-steel housing |
| Membrane types | Various tubular UF membrane options from leading manufacturers |
| Membrane area | 104 – 666 m² |
| Configuration | 2 to 8 parallel module passes, 10 to 16 modules in series, 20 to 128 modules in total |
| Performance | up to 56'600 l/h (apple juice, 12 °Bx, 50 °C) |
| Temperature range | 10 – 55 °C |
| pH range | 2.0 – 10.5 |
| Connected load | 57 – 133 kW |
| Dimensions | L × B × H = 3’650 bis 6’010 x 4’750 x 3’420 mm |
| Scope of supply | Circulation unit with control cabinet assembled on frame, filter module unit, fully automated PLC control with touch panel. |